Ground racks are used when tooth accuracy and surface finish need to be tighter than a normal milled finish can economically provide. Milled racks remain appropriate for many robust motion systems, and induction hardening can add wear resistance without automatically requiring tooth grinding.
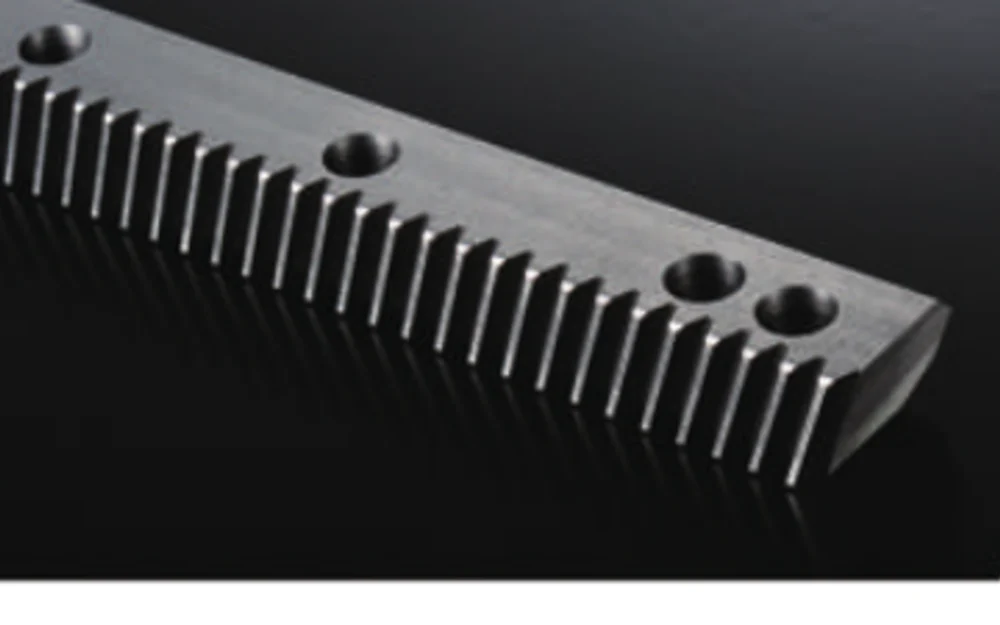
Grinding changes the tooth finish, not the whole machine
Grinding can improve pitch consistency and tooth-flank surface condition after heat treatment. Its value is most visible in systems that care about repeatable positioning, smooth reversal, running quality or a controlled tooth finish.
It does not compensate for a flexible machine base, poor rack joints, a loose gearbox or incorrect pinion alignment. A ground rack should therefore be specified together with the accuracy target for the axis, not as an isolated premium feature.
What a milled rack does well
A milled rack can transmit load reliably and can be combined with suitable material and heat treatment for wear resistance. Material handling, lifting, robust automation and many general machine axes do not need a ground tooth surface if the functional tolerance and running requirement are satisfied by milling and the selected heat-treatment route.
Compare by requirement, not by price alone
| Positioning requirement | Tighter or more sensitive positioning may justify ground teeth; general positioning may not. |
|---|---|
| Speed and reversal | High speed and frequent reversals make running smoothness more important. |
| Wear | Heat treatment and lubrication strongly affect wear; grinding is not a substitute for correct hardness or lubrication. |
| Noise | Tooth finish and mesh quality influence noise, but gearbox, structure and lubrication also contribute. |
| Cost | Grinding adds process steps; use it where the machine receives real functional value. |
| Inspektion | Higher accuracy usually means more controlled tooth inspection and a clearer datum/tolerance scheme. |
Heat treatment belongs in the same decision
Induction hardening, carburizing or other treatments can change wear resistance and distortion behaviour. The order of heat treatment and finishing should match the intended material and accuracy route. If hardness depth or final tooth hardness is controlled, it belongs on the drawing or purchase specification.
Do not copy a hardness value from an unrelated rack series. The correct requirement depends on material, load, wear target and the manufacturing process.

Selection shortcut
Start from the machine tolerance and duty, then ask what finish is needed to support it. A precision machine tool may justify ground racks. A material-handling axis may not. A high-speed cutting machine can sit between the two depending on its accuracy target and the rest of the drive system.
Senden Sie die Details, die das Teil definieren.
Ein aussagekräftiges Angebot beginnt mit der Geometrie und dem Betriebskontext. Senden Sie die Zeichnung, die Stückzahl und die Anforderungen an die Regelung; bei zahnstangengetriebenen Achsen fügen Sie bitte, falls vorhanden, Informationen zu Verfahrweg, Geschwindigkeit, Beschleunigung, Last und dem zugehörigen Ritzel oder Getriebe hinzu.
Bestellung: Die Mindestbestellmenge (MOQ) ist je nach Produkttyp und Bestellwert flexibel. Geeignete Muster für Neukunden umfassen 1–5 Stück; Bestellungen mit gemischten Modellen werden ab einem Gesamtwert von ca. 1.500 USD unterstützt, während Bestellungen von 1–2 Stück zu einem höheren Stückpreis möglich sind.
Timing & terms: Standardteile werden üblicherweise innerhalb von 10-25 Werktagen geliefert, kundenspezifische Komponenten innerhalb von 20-45 Werktagen und Projektausrüstung innerhalb von 45-120 Werktagen. EXW, FOB, CIF und DAP sind gängige Lieferbedingungen; FCA, CFR, CPT, CIP und DDP können im Einzelfall besprochen werden.