Sun Gear Manufacturing for Drawing-Based Projects
Manufacturing routes are selected from the tooth geometry, interface, material, heat treatment and required quality of the ordered sun gear or planetary component.
Start with the released tooth definition and functional datums.
A useful manufacturing review identifies the blank route, soft machining, gear-cutting method, heat-treatment sequence, hard finishing and inspection before production starts. The bore, spline or shaft features need to stay connected to the tooth datum strategy throughout that sequence.
Send drawing & planetary data
PDF/STEP, revision, quantity, application and any available mating-gear information.
Confirm tooth geometry
Module/DP, tooth count, pressure angle, spur/helical form, helix angle and hand.
Confirm interfaces
Bore, spline, shaft, journals, shoulders and functional datum relationships.
Plan material & treatment
Keep material, carburizing/nitriding/hardness and case requirements tied to the approved design.
Manufacture & hard-finish
Sequence turning, gear cutting, spline work, heat treatment and grinding as required.
Inspect controlled features
Check tooth geometry together with bore/spline/journal and face relationships.
Pack & ship
Export packing and the agreed Incoterm for the released quantity.
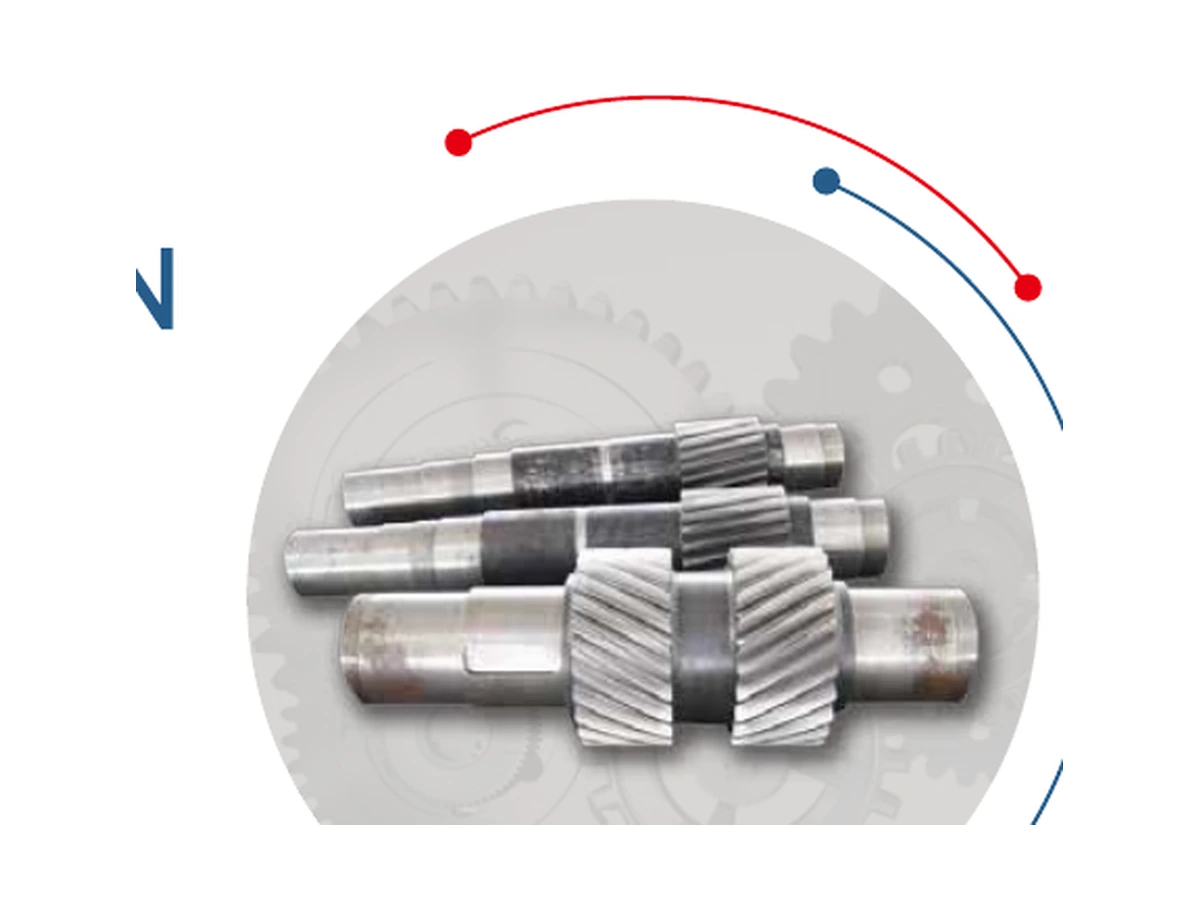
External teeth, internal teeth and splines require different access.
Sun gears are commonly external spur or helical gears, so hobbing and related generating processes are natural options when the geometry allows. Shoulders, clustered features or very short clearances can change tool access. Internal splines and ring gears may require shaping, broaching, skiving or another process selected for the geometry and volume.
The manufacturing method is not chosen from the product name alone. A drawing review is needed before a firm route is quoted.
Plan the sequence around distortion and the required tooth surface.
Industrial sun gears may use carburizing, nitriding, induction hardening, through-hardening or quenched-and-tempered conditions depending on material and duty. If tooth grinding or journal grinding is required after heat treatment, stock allowance and datum recovery are built into the process plan.
| Soft machining | Blank preparation, turning, drilling and interface machining before hardening |
|---|---|
| Gear cutting | Hobbing/shaping or an equivalent process selected for geometry and access |
| Spline processing | Broaching, shaping, skiving or other route according to spline form and volume |
| Värmebehandling | Drawing-specified case/core or through-hardening route |
| Hard finishing | Gear grinding, bore/journal grinding or other finishing where specified |
| Final inspection | Gear geometry plus bore/spline/journal and face relationships to functional datums |
Low-volume and series work need different production economics.
Small prototype quantities may favor flexible tooling and measurement setups. Repeat programs can justify dedicated fixtures, gauges and process controls. Tell us both the first-order quantity and the expected annual or batch demand so the route can be reviewed commercially as well as technically.